CNC Machining PEEK: Feeds, Speeds, Annealing Cycles & Precision Tooling Guidelines

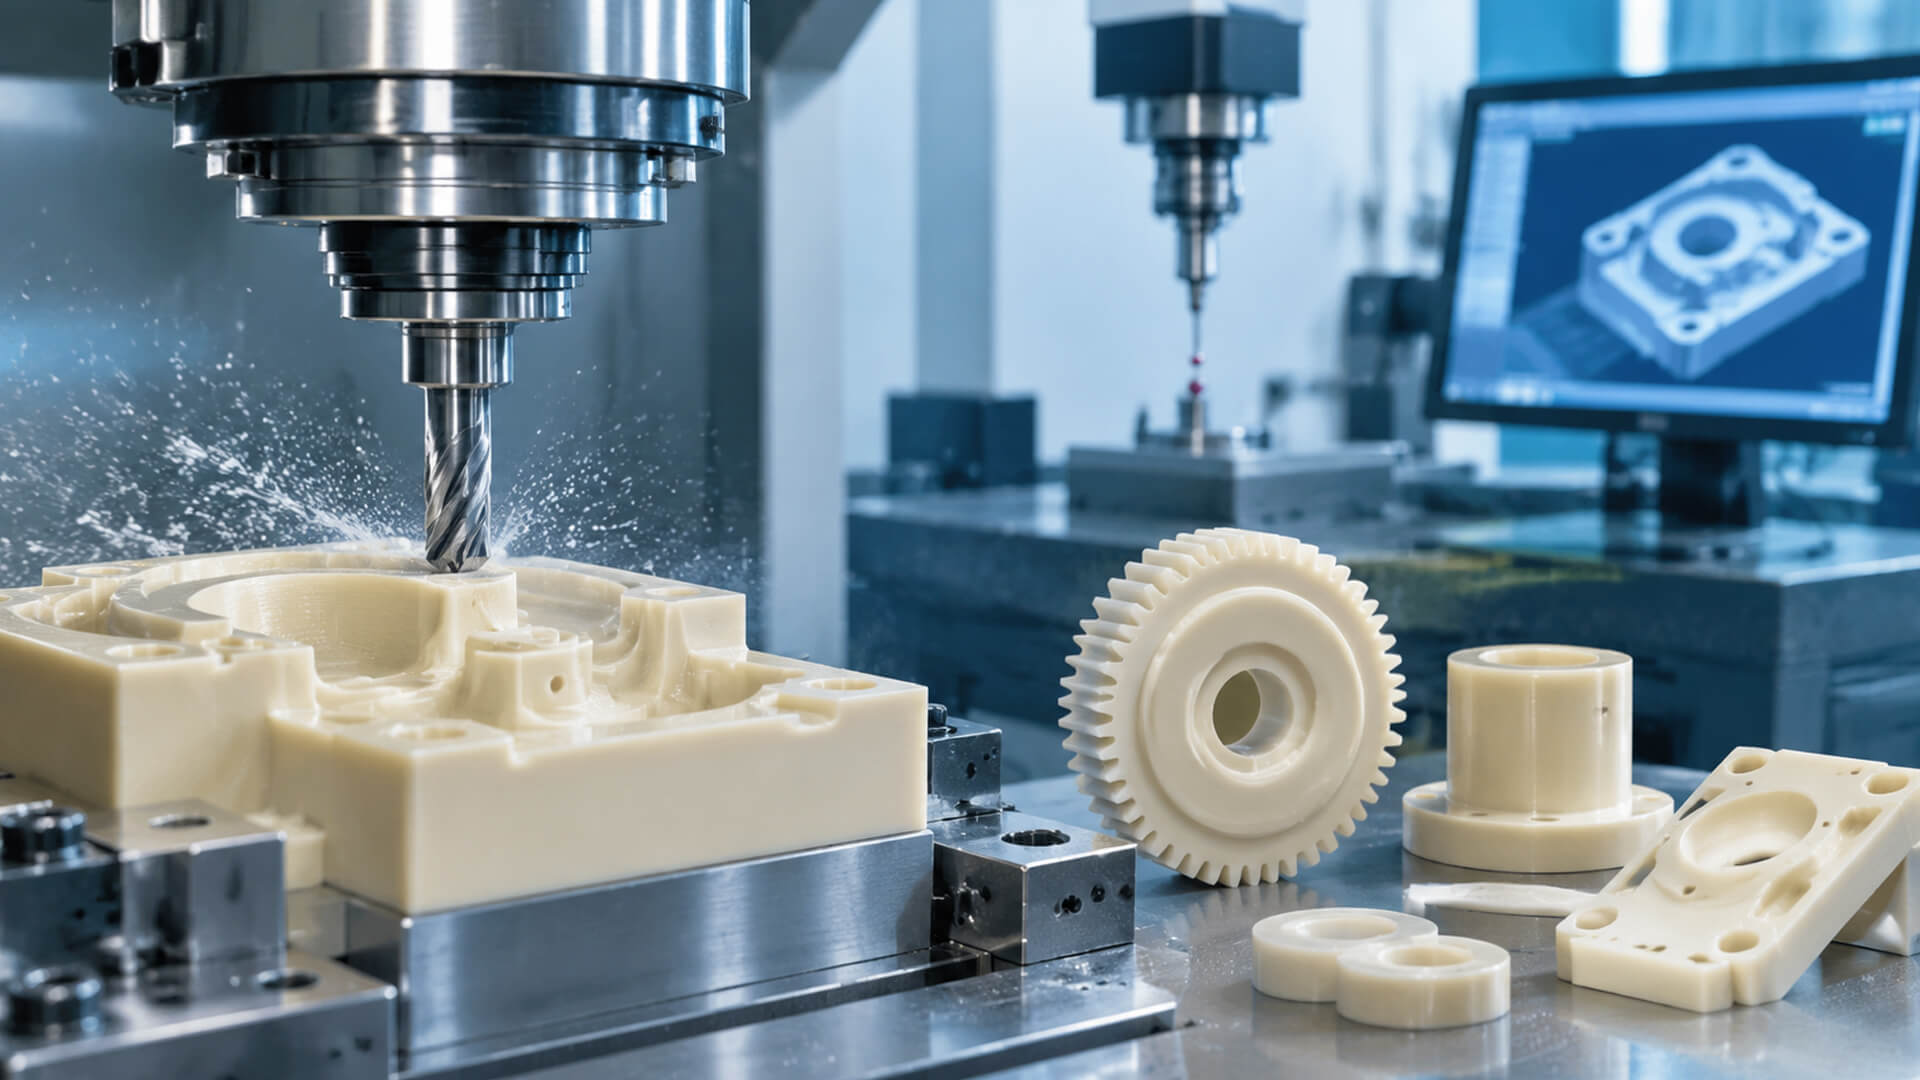
Polyetheretherketone (PEEK) represents an engineering paradox in subtractive manufacturing. With a tensile strength exceeding 100 MPa, continuous operating temperatures up to 250°C (482°F), and exceptional chemical resistance, it frequently replaces titanium, stainless steel, and aluminum alloys in critical aerospace, semiconductor, and medical applications.
However, translating these bulk material properties into precision components requires an entirely different mechanical approach than machining metals.
Unlike metals, which dissipate cutting energy primarily through shear plane heat deformation into the chip, PEEK exhibits an extremely low thermal conductivity of approximately 0.25 W/(m⋅K) (compared to ~200 W/(m⋅K) for 6061-T6 aluminum and ~16 W/(m⋅K) for 304 stainless steel). Because heat cannot quickly transfer into the tool or workpiece, it accumulates directly at the cutting zone.
Combined with a relatively low glass transition temperature (Tg≈143°C/289°F) and a melting point of 343°C(649°F), unoptimized speeds, feeds, or tool geometries instantly trigger localized melting, tool gumming, elastic deflection, and catastrophic micro-cracking driven by residual tensile stresses.
| Thermal Conductivity Comparison | |
|---|---|
| 6061-T6 Aluminum | ~200 W/(m·K) |
| 304 Stainless Steel | ~16 W/(m·K) |
| Virgin PEEK | ~0.25 W/(m·K) Heat Trapped |
Machining behavior diverges further depending on the specific PEEK grade:
- Unfilled / Virgin PEEK (e.g., Victrex 450G, Ketron 1000): Exhibits high elongation at break (up to 40%). It produces long, continuous, ductile ribbon chips that tend to wrap around spinning tool shanks, generate high frictional burrs, and push away from the cutting edge via viscoelastic recovery.
- 30% Glass-Filled PEEK (GF30): Drastically increases dimensional stiffness and flexural modulus while lowering thermal expansion. However, the embedded, randomly oriented glass micro-fibers act as severe abrasives, causing rapid abrasive flank wear on conventional carbide tooling within minutes.
- 30% Carbon-Filled PEEK (CF30): Offers superior mechanical stiffness, thermal conductivity, and ESD dissipation, but exhibits anisotropic shear resistance and extreme brittleness at component edges, leading to edge chipping and rapid micro-fractures if cutting edges lose their absolute sharpness.
Navigating these material dynamics requires validated feeds and speeds, thermal management via structured annealing cycles, rigid workholding, and advanced multi-axis machining capabilities.
Table of Contents
Recommended Speeds, Feeds & Cutting Parameters
PEEK must be cut cleanly by shearing rather than displaced by compressive plowing. Running spindle speeds too fast relative to the feed rate generates excessive rubbing and frictional heat; running feed rates too high without adequate rake clearance overloads the polymer core, inducing sub-surface micro-fractures.
The following parameter matrices provide verified starting points for milling and turning operations across Virgin, GF30, and CF30 PEEK.
Milling Parameters (End Milling & Slotting)
| Operation / Grade | Cutting Speed (SFM) |
Cutting Speed (m/min) |
Chip Load (mm/tooth) |
Axial DOC (ap) |
Radial WOC (ae) |
|---|---|---|---|---|---|
| Virgin PEEK (450G) - Roughing | 400 – 700 | 120 – 210 | 0.08 – 0.15 | Up to 1.0 × D | 0.4 – 0.6 × D |
| Virgin PEEK (450G) - Finishing | 600 – 900 | 180 – 275 | 0.03 – 0.06 | 0.1 – 0.25 × D | 0.05 – 0.1 × D |
| PEEK GF30 - Roughing | 250 – 450 | 75 – 135 | 0.05 – 0.10 | Up to 0.75 × D | 0.3 – 0.5 × D |
| PEEK GF30 - Finishing | 350 – 550 | 105 – 170 | 0.02 – 0.05 | 0.1 – 0.2 × D | 0.05 – 0.1 × D |
| PEEK CF30 - Roughing | 300 – 500 | 90 – 150 | 0.06 – 0.12 | Up to 0.75 × D | 0.3 – 0.5 × D |
| PEEK CF30 - Finishing | 400 – 650 | 120 – 200 | 0.03 – 0.05 | 0.1 – 0.2 × D | 0.05 – 0.1 × D |
Turning Parameters (OD & Boring)
| Material & Cut Type | Surface Speed (SFM) |
Surface Speed (m/min) |
Feed Rate (mm/rev) |
Depth of Cut (DOC - mm) |
Nose Radius (mm) |
|---|---|---|---|---|---|
| Virgin PEEK (450G) Roughing | 450 – 750 | 140 – 230 | 0.15 – 0.30 | 1.50 – 3.50 mm | 0.4 – 0.8 mm |
| Virgin PEEK (450G) Finishing | 650 – 950 | 200 – 290 | 0.05 – 0.12 | 0.25 – 0.75 mm | 0.2 – 0.4 mm |
| PEEK GF30 / CF30 Roughing | 300 – 500 | 90 – 150 | 0.10 – 0.20 | 1.00 – 2.50 mm | 0.4 mm |
| PEEK GF30 / CF30 Finishing | 450 – 700 | 140 – 215 | 0.04 – 0.08 | 0.20 – 0.50 mm | 0.2 mm |
Tooling Selection: Carbide vs. Polycrystalline Diamond (PCD)
Tool geometry dictates whether PEEK shears cleanly or plastically deforms during machining. Standard off-the-shelf end mills engineered for steel or hardened alloys feature hone-dulled cutting edges (edge radii of 15–30 µm) designed to resist chipping under heavy shock loads. In PEEK, this rounded cutting edge generates destructive compressive forces, thermal expansion, and severe burr formation.
Carbide Tool Geometry for PEEK
Milling & TurningUnfilled Virgin PEEK Tooling
- Sub-micron Grain Uncoated Carbide: Use micro-grain solid tungsten carbide (WC-Co) ground to a razor-sharp edge (edge radius <5μm).
- Aggressive Geometries: Utilize positive rake angles (+10° to+15°) and large clearance angles (+12° to+18°) to eliminate rubbing along the tool flank.
- Polished Flutes: Flute surfaces must feature an optical mirror finish (Ra<0.1μm) to reduce friction and evacuate ductile ribbon chips without clogging.
Reinforced PEEK (GF30 & CF30) Tooling
- Polycrystalline Diamond (PCD): Glass and carbon fibers wear standard carbide edges within minutes. Once the edge radius dulls past 10μm, cutting temperatures spike rapidly. PCD tooling maintains an edge up to 50 times longer than uncoated carbide.
- PCD Diamond Grain Sizing: Choose medium grain sizes (2 µm to 10 µm). Smaller grain sizes permit sharper primary cutting edges, whereas coarser grains provide superior impact toughness during interrupted cuts.
- Diamond-Like Carbon (DLC) Coatings: For complex small-diameter end mills (<1.5 mm) where PCD brazing is impractical, multi-layer hydrogen-free DLC (ta-C) coatings provide a very low coefficient of friction (μ≈0.05−0.1) combined with exceptional micro-hardness (>50 GPa).
Coolant Strategy: Pure Cold Air vs. Flood Coolant
- Medical & Semiconductor Components: Coolant additives often penetrate the amorphous inter-spherulitic regions of PEEK, leaving behind trace hydrocarbons, chlorides, or sulfur compounds that cause outgassing or biocompatibility failures. For these components, dry machining with high-pressure vortex cold-air guns (-10°C to 0°C) is mandatory.
- Industrial Applications: When surface finish and extreme cycle times take precedence, water-soluble, chlorine-free emulsion coolants are acceptable. Never use straight cutting oils; their viscosity impedes localized heat transfer, and hydrocarbon-based additives induce environmental stress cracking (ESC) in PEEK components under tension.
The 3-Stage PEEK Annealing Process
During extrusion or injection molding, PEEK develops severe internal stress gradients caused by differential cooling between outer surfaces and the center core. If a machine shop skips preliminary heat treatment and removes extensive material, these locked-in internal stresses re-equilibrate, warping the part.
The 3-Stage PEEK Annealing Timeline
Stress Relief CycleTo achieve and retain critical dimensions (<±0.010 mm), implement a 3-Stage Annealing Protocol:
- Pre-Machining Annealing: Applied to raw bar stock or extruded plates before cutting to relieve initial extrusion stresses and homogenize crystallinity.
- Intermediate Annealing: Performed after roughing operations (leaving 0.5–1.0 mm of stock on critical faces). This relieves cutting-induced tensile stresses before finishing passes.
- Final Stress Relief: Applied after finishing operations to ensure long-term structural stability across operational thermal cycles.
| Annealing Phase | Ramp-Up Rate | Soak Temperature | Dwell / Soak Duration | Ramp-Down Rate |
|---|---|---|---|---|
| Stage 1: Pre-Machining | +10°C to +15°C / hr up to 140°C; then +10°C / hr to 250°C | 250°C (482°F) | 1 hr per 6 mm (0.25 in) of cross-sectional wall thickness | -10°C / hr down to 140°C (Tg); then power-off oven cool to < 50°C |
| Stage 2: Intermediate (Post-Roughing) |
+15°C to +20°C / hr | 200°C – 220°C | 1 hr per 10 mm (0.40 in) of semi-machined wall section | -10°C / hr down to 120°C; slow natural ambient cool down to room temp |
| Stage 3: Final Stabilization (Post-Finishing) |
+10°C / hr | 150°C – 160°C | 2 to 4 hours static dwell | -8°C / hr continuous slow cooling down to 40°C |
Crucial Process Note: Never open the annealing oven door prematurely. Exposing parts at 200°C to room-temperature ambient drafts produces instantaneous crystalline shock, freezing the outer skin while the core contracts, which can warp or split precision parts.
Machining Challenges & Shop-Floor Solutions
Deep-Hole Drilling: Chip Packing and Workpiece Splitting
Standard twist drills with 30° helix angles quickly pack ductile, stringy PEEK chips into their flutes. Friction multiplies down the hole, melting the polymer and snapping drill bits or causing hydraulic blowout at the exit hole.
PEEK Deep-Hole Drilling Rules
Chip Evacuation Protocol- Tool Geometry: Use parabolic flute drills with a low helix angle (15°−20°) to eject continuous chips up and out of the cut. Maintain a point angle between 118° and 130° with thinned webs to minimize center thrust.
- Kinematic Strategy: Implement an aggressive full-retract peck drilling cycle (G83). Program peck depths of no more than 0.5×D to 1.0×D, fully retracting the tool outside the hole to dislodge stringer chips with an external air blast before re-entering.
Thin-Wall Part Clamping: Compressive Elastic Deformation
PEEK exhibits an elastic modulus of ~3.8 GPa—roughly 5% of aluminum’s stiffness (~70 GPa). When clamped with standard serrated steel vise jaws, the polymer easily compresses.
The part is machined true while compressed, but springs back into an out-of-round oval or warped geometry once released from the fixture.
- Soft Jaws and Pie Jaws: Machine full-contact aluminum soft jaws or wrap-around 360° pie jaws on lathes to distribute clamping forces evenly across the component.
- Vacuum Fixturing: For delicate manifold plates or semiconductor wafer retainers with wall thicknesses below 1.5 mm, use porous ceramic vacuum chucks to apply uniform downward pressure across the entire part face, completely eliminating mechanical clamping distortion.
- Single-Setup 5-Axis Machining: Utilizing multi-axis machines like our Hermle C400 and DMG MORI DMU 50 allows us to machine 5 faces of complex geometric housings in a single fixture clamping. By reducing multiple reclamping setups down to one, we eliminate cumulative datum stack-up errors and prevent stress-induced geometric distortion.
Micro-Feature Milling Without Thermal Smearing
For complex micro-fluidic channels and micro-pins common in medical diagnostic equipment:
- Utilize ultra-precision high-speed mills, such as our Beijing Jingdiao JDGR200T, equipped with a 24,000 RPM high-speed, direct-drive spindle.
- The combination of extremely low dynamic spindle runout (<1μm) and high-speed CNC control feeds micro-endmills cleanly below the elastic threshold of PEEK. This yields mirror-like surface finishes (Ra≤0.2μm) and sharp corners without mechanical burring.
Precision Inspection & Quality Verification
Verifying micro-tolerances on PEEK components requires metrology setups tailored to polymer physics. The primary inspection trap with PEEK stems from its high Coefficient of Linear Thermal Expansion (CLTE):
CLTE(Virgin PEEK) ≈ 47 – 55 × 10⁻⁶ / K
Compare this to 6061 Aluminum at ≈ 23 × 10⁻⁶ / K and Structural Steel at ≈ 12 × 10⁻⁶ / K.
A temperature change of just 5°C on an uninsulated shop floor causes a 100 mm PEEK feature to expand by approximately:
ΔL = 100 mm × (50 × 10⁻⁶ / K) × 5 K = 0.025 mm (0.001″)
That thermal expansion alone consumes the entire tolerance band of a precision component, which is why temperature-stabilized metrology is essential.
| Thermal Drift on a 100mm Feature (ΔT = 5°C / 9°F) | |
|---|---|
| Structural Steel | ~0.006 mm drift |
| 6061-T6 Aluminum | ~0.011 mm drift |
| Virgin PEEK |
~0.025 mm drift
Thermal Trap
|
Climate-Controlled QA Lab (20°C±1°C)
At Celerity Precision, all PEEK parts are transferred into our dedicated metrology laboratory and soaked for a minimum of 4 to 8 hours until their internal core temperature stabilizes at 20°C±1°C(68°F±1.8°F).
Zeiss Coordinate Measuring Machines (CMM)
Spatial dimensional verification is conducted using our bridge-type Zeiss CMM.
- Probing speed, deceleration, and contact force are calibrated to prevent stylus tip penetration into soft polymer skins.
- Critical bore diameters and true positional tolerances are confirmed down to ±0.005 mm (
±0.0002′′±0.0002′′). - Non-contact video measurement systems and high-accuracy digital height gauges are deployed for thin-walled sections susceptible to contact probe deflection.
Material Authenticity Verification via XRF Spectroscopy
A growing issue in high-performance polymer procurement is counterfeit, off-spec, or regrind-contaminated material. Subcontractors sometimes blend recycled PEEK scrap into virgin billets, degrading yield strength, electrical insulation, and chemical resistance.
Celerity Precision validates raw material stock using an X-Ray Fluorescence (XRF) Spectrometer / Analyzer:
- Each material lot undergoes elemental spectroscopic profiling to screen for heavy-metal impurities, halogenated contamination, and non-conforming filler formulations.
- Every production order is cross-checked against raw mill certificates and shipped with a comprehensive Material Authenticity & Traceability Certification, guaranteeing 100% prime virgin polymer resin suitable for medical and aerospace service.
DFM Tips to Reduce PEEK Machining Costs
Raw extruded PEEK stock costs roughly 30 to 50 times more than standard 6061-T6 aluminum by weight. Poor Design for Manufacturability (DFM) drives up expenses through extended cycle times, tool wear, and scrap rates.
Applying these four design guidelines will help minimize your overall production costs:
| Design Consideration | The Cost Trap | Recommended Engineering Practice |
|---|---|---|
| 1. Minimum Wall Thickness | Walls < 0.8 mm (0.030") flex under tool pressure, requiring micro-step downpasses and slow feed rates to prevent chatter and distortion. | Maintain wall thickness ≥ 1.20 mm (0.048") wherever possible. If thin fins are essential, specify supporting rib structures to enhance local rigidity. |
| 2. Internal Corner Radii | Sharp internal corners (R < 0.5 mm) create stress concentration points where micro-cracks propagate, while forcing the use of delicate, easily broken micro-cutters. | Design internal cavity radii to at least R ≥ 1/3 of cavity depth. This allows the use of rigid, larger-diameter tooling, speeding up cycle times. |
| 3. Thread Engagement Depth | Specifying thread depths greater than 2.5× the nominal diameter risks chip packing, binding, and tool breakage during tapping operations. | Limit thread depths to 1.5× to 2.0× diameter. Because PEEK absorbs stresses elastically, deeper thread engagements offer negligible additional pullout strength. |
| 4. Non-Functional Roughness | Specifying Ra 0.2 µm (8 µin) finishes across all non-critical surfaces drives up cycle times and requires costly secondary polishing. | Target Ra 0.8 to 1.6 µm (32 to 63 µin) on non-functional surfaces, reserving tight sub-micron surface finishes exclusively for dynamic sealing and bearing interfaces. |
Precision Machining Services for Mission-Critical PEEK Components
Engineering successful PEEK components requires matching real-world polymer science with rigid CNC machine tools, specialized cutters, and climate-controlled metrology.
Whether your design calls for complex geometries cut via 5-axis CNC milling or volume runs supported by custom PEEK CNC machining services, Celerity Precision delivers repeatable, tight-tolerance parts backed by comprehensive inspection reports.
Have a Challenging PEEK Project Requiring Tight Tolerances?
Send us your 3D CAD models (STEP, IGS) and 2D engineering drawings. Our engineering team will deliver a comprehensive, complimentary DFM review and quotation within 24 hours—covering stress relief, tooling strategy, and critical-feature tolerance validation.

CP Engineering Team
Authored and peer-reviewed by the Senior Engineering and Metrology Team at Celerity Precision. Backed by German 5-axis CNC machining centers, high-speed micro-milling platforms, and a climate-controlled Zeiss CMM inspection lab, our team delivers deep DFM insights, material machinability guides, and precision manufacturing solutions for aerospace, medical, and semiconductor developers worldwide.