How to Machine Inconel 718: Speeds, Feeds, Ceramic Tooling & Work-Hardening Solutions

Inconel 718 (UNS N07718, W.Nr. 2.4668) is a precipitation-hardenable nickel-chromium-iron superalloy engineered for environments where high tensile, creep, and rupture strength must be retained under temperatures up to 700°C (1,290°F), coupled with resistance to high-pressure oxidation and pitting corrosion. With a chemical composition anchored by 50.0% to 55.0% nickel, 17.0% to 21.0% chromium, 4.75% to 5.50% niobium plus tantalum, and 2.80% to 3.30% molybdenum, Inconel 718 derives its primary mechanical properties from the coherent precipitation of body-centered tetragonal gamma double prime (γ′′−Ni₃Nb) and face-centered cubic gamma prime (γ′−Ni₃(Al, Ti)) phases within an austenitic face-centered cubic (γ) nickel matrix.
While these metallurgical characteristics make Inconel 718 irreplaceable for aircraft turbine disks, rocket engine combustion components, nuclear reactor core internals, and high-pressure deep-sea downhole completion equipment, they also place the alloy among the most difficult materials to machine in precision manufacturing.
Subtractive processing of Inconel 718 is governed by three severe physical barriers:
First, Inconel 718 possesses an exceptionally low thermal conductivity of approximately 11.4 W/(m·K) at room temperature (climbing marginally to ~14.6 W/(m·K) at 400°C), compared to ~50 W/(m·K) for medium carbon steel and ~160 W/(m·K) for standard aluminum alloys. In ordinary alloy cutting, the ejected chip absorbs the majority of the thermal energy generated in the primary shear zone. In Inconel 718, heat cannot dissipate rapidly into the chip or the parent workpiece. As a result, thermal energy concentrates along the narrow tool-chip contact zone and the primary cutting edge. Cutting zone temperatures frequently exceed 1,000°C (1,832°F), causing rapid thermal degradation, thermal softening of carbide binders, and rapid crater wear on the tool rake face.
Second, the alloy maintains high yield strength and shear resistance at elevated cutting temperatures. In standard steels, localized frictional heat induces thermal softening ahead of the tool, lowering cutting forces. Inconel 718 resists thermal softening up to 650°C. The specific cutting force required to shear the alloy remains high (k_c≈2,800 to3,200 N/mm², more than double that of structural steel). This extreme mechanical load is exerted over a microscopic contact area, producing localized compressive stresses along the cutting wedge that exceed 1,500 MPa.
Third, Inconel 718 exhibits an aggressive work-hardening rate. When subjected to plastic shear strain, its austenitic crystal structure generates high dislocation densities that multiply rapidly. If cutting tool geometries or machining feeds allow the tool edge to rub, burnish, or drag across the material surface rather than cleanly shearing beneath it, the surface layer instantly strain-hardens from its baseline annealed state of 36–40 HRC to a brittle hardness exceeding 50–55 HRC. Subsequent cutting passes attempting to engage this cold-worked layer experience catastrophic micro-chipping, depth-of-cut notch wear, and sudden tool fracture.
Overcoming these metallurgical failure modes requires specialized toolpath kinematics, application-specific tool substrates (advanced sub-micron carbides versus whisker-reinforced ceramics), rigid multi-axis machine platforms, and optimized cooling strategies. Engineering teams developing mission-critical components can leverage Celerity Precision’s advanced machining platforms through our custom Inconel CNC machining services.
Table of Contents
The Mechanism of Work Hardening & How to Stop It
Work hardening (strain hardening) represents the primary failure point in Inconel 718 production. Understanding its metallurgical mechanics is essential to prevent rapid tool failure and scrapped components.
During mechanical shearing, the face-centered cubic (FCC) nickel-iron matrix experiences localized plastic flow. Under the influence of the cutting tool’s edge radius, the plastic deformation zone extends ahead of the cutting edge and downward beneath the machined surface. This localized strain produces rapid dislocation tangles, stacking faults, and grain boundary pile-ups within the austenitic grains. The mechanical consequence is that the top 0.02 mm to 0.08 mm of the cut surface becomes significantly harder, stronger, and more abrasive than the parent material.
To stop work hardening from destroying tools, machine shops must adhere to four core machining rules:
1. The Penetration Rule: Cut Below the Work-Hardened Zone
The depth of cut (a_p) and feed per tooth (f_z) must always be programmed to penetrate beneath the cold-worked boundary layer formed by the previous toolpass.
- Axial Depth Rule: For semi-finishing and finishing milling passes, the axial depth of cut (a_p) should never be set below 0.20 mm (0.008″). Light skim cuts of 0.05 mm (0.002″) force the tool edge to rub directly against the strain-hardened skin of the preceding pass, causing abrasive flank wear and edge destruction within seconds.
- Feed per Tooth Minimum: Maintain a positive chip load. For carbide end milling, minimum feed per tooth must stay above 0.035 mm/tooth (0.0014 IPT). Taking a lighter feed causes the tool cutting radius to burnish rather than shear the stock, generating intense friction and expanding the depth of the work-hardened zone.
2. Strictly Eliminate Tool Dwell and Zero-Feed Rubbing
A rotating cutting tool must never pause, dwell, or hesitate while in contact with Inconel 718.
- Holemaking and Drilling: Never program a dwell (G04) at the bottom of a hole during drilling, boring, or counterboring. The moment the tool rotates without advancing, the cutting edges burnish the bottom of the bore, creating a glazed, work-hardened surface that dulls or breaks the tool during subsequent reaming, tapping, or drill-point re-entry.
- Tool Entry and Exit: Program tangential arc-in and arc-out toolpaths. Plunging straight down along the Z-axis causes tool deflection, localized dwelling, and severe center-edge chipping. Helical ramping or ramp ramping at gentle angles (between 1.0° and 2.5°) ensures a continuous chip load and smooth tool engagement.
- Peck Drilling Cycles: Avoid standard G83 peck drilling where the drill fully retracts out of the hole and feeds back in to touch the glazed bottom. Use controlled high-pressure through-tool coolant with specialized drill geometries that clear chips in a single continuous peck or employ micro-peck cycles that never let the tool lose forward momentum against the cut face.
3. Maintain Continuous Climb Milling (Down Milling)
Climb milling (down milling) is non-negotiable for Inconel 718.
In conventional milling (up milling), the cutting tooth enters the cut at zero chip thickness, rubbing and skidding across the work-hardened surface until sufficient pressure builds to initiate a shear cut, exiting at maximum chip thickness. This initial rubbing phase generates high frictional heat and work-hardens the surface for the next entering tooth.
In climb milling, the tooth engages the material at maximum chip thickness, immediately biting beneath the work-hardened surface layer and carrying cutting heat forward into the chip. The tooth then thins out to zero thickness as it exits the cut, minimizing abrasive dragging across the newly machined face.
Feeds, Speeds & Cutting Parameters
Machining Inconel 718 requires two distinct operational tracks depending on production volume, feature geometry, and machine kinematics: the Micro-Grain Carbide Track (engineered for precision finishing, tight tolerances, and delicate structural walls) and the Whisker-Reinforced Ceramic Track (engineered for high-speed volumetric roughing and pocket hogging).
The following engineering parameter matrix presents verified baseline cutting data for both approaches across solution-annealed and precipitation-aged Inconel 718 (36 to 44 HRC):
| Machining Operation | Tooling Substrate & Coating | Speed (SFM) |
Speed (m/min) |
Chip Load / Feed (FPT / IPR) |
Radial (Ae) | Axial (Ap) |
|---|---|---|---|---|---|---|
| End Milling - Roughing Carbide | Sub-micron Carbide (AlCrN/AlTiN) | 70 – 120 | 22 – 38 | 0.04 – 0.08 mm/tooth | 0.25 – 0.40 × D | 0.50 – 1.00 × D |
| End Milling - Finishing Carbide | Sub-micron Carbide (PVD TiAlN) | 100 – 160 | 30 – 50 | 0.025 – 0.05 mm/tooth | 0.05 – 0.10 × D | 1.00 – 1.50 × D |
| End Milling - Ceramic Ceramic | SiCw Whisker-Reinforced Ceramic | 600 – 1,000 | 180 – 305 | 0.025 – 0.06 mm/tooth | 0.10 – 0.20 × D | 0.50 – 1.00 × D |
| Face Milling - Carbide Carbide | Indexable Inserts (PVD AlTiN/TiCN) | 80 – 140 | 25 – 42 | 0.08 – 0.14 mm/tooth | 0.60 – 0.75 × D | 1.00 – 2.00 mm |
| Face Milling - Ceramic Ceramic | Round Ceramic Inserts (RNGN/RPGN) | 700 – 1,200 | 215 – 365 | 0.05 – 0.12 mm/tooth | 0.50 – 0.70 × D | 0.75 – 1.50 mm |
| Turning - Roughing Carbide | ISO Carbide (PVD TiAlN / TiCN) | 90 – 150 | 28 – 45 | 0.12 – 0.25 mm/rev | N/A | 1.00 – 2.50 mm |
| Turning - Finishing Carbide | ISO Carbide (Uncoated or TiAlN) | 120 – 180 | 36 – 55 | 0.05 – 0.10 mm/rev | N/A | 0.20 – 0.50 mm |
| Turning - Ceramic Ceramic | Whisker Ceramic / Sialon | 550 – 850 | 170 – 260 | 0.08 – 0.16 mm/rev | N/A | 0.80 – 1.80 mm |
| Trochoidal Milling HEM Strategy | High-Performance Solid Carbide | 150 – 240 | 45 – 75 | 0.06 – 0.12 mm/tooth | 0.05 – 0.08 × D | 2.00 – 3.00 × D |
Dynamic Trochoidal Milling Strategy Guide
Dynamic milling (high-efficiency milling – HEM) alters the thermal dynamics of cutting Inconel 718 with solid carbide end mills. Instead of taking traditional heavy radial stepovers (40% to 50% Ae) at slow speeds, dynamic milling combines light radial engagements with deep axial cuts and high feed rates.
The operational parameters for dynamic milling in Inconel 718 rely on three kinematic principles:
- Light Radial Stepover (Ae = 5% to 8% of Cutter Diameter): By restricting radial engagement to under 8%, the radial arc of contact drops to less than 30 degrees per tool revolution. This brief contact window reduces the heating cycle of each individual flute, followed by an extended non-cutting cooling window in which high-pressure coolant washes the cutting edge before it re-engages.
- Chip Thinning Compensation: Because light radial stepovers produce a chip whose maximum thickness is substantially thinner than the programmed linear advance per tooth, machinists must adjust programmed feeds. Use the chip thinning equation to calculate the adjusted table feed rate (v_f):
Adjusted Feed per Tooth = Target Chip Thickness / Square Root of (Radial Width of Cut / Cutter Diameter)
Maintaining a consistent target chip thickness (typically 0.04 mm to 0.06 mm) prevents the tool edge from rubbing in the light-engagement zone, eliminating rapid work hardening.
- Extended Axial Depth (Ap = 2.0 to 3.0 × D): Utilizing the full length of the end mill’s flutes spreads cutting forces and thermal stresses across a larger surface area of the carbide substrate. Rather than concentrating flank wear and notch wear exclusively on the bottom 2 mm of the cutter, wear distributes evenly along the flute length, boosting usable tool life by 200% to 400% while increasing overall metal removal rates (MRR).
Tooling Substrates, Edge Preparation & Coatings
Selecting the correct cutting tool substrate, micro-geometry, and surface coating is critical to managing Inconel 718’s high specific cutting energy and thermal concentration.
1. Solid Carbide Tooling Substrates
For carbide tooling, standard C-2 or general-purpose C-5 grades fail quickly due to thermal fracturing and micro-grain pullout.
- Sub-Micron Tungsten Carbide: Specify ultra-fine or sub-micron grain tungsten carbide (WC) with grain sizes between 0.4 µm and 0.8 µm, bound with 8% to 10% cobalt (Co). The fine grain structure maximizes transverse rupture strength (TRS > 4,200 MPa) while maintaining high hot-hardness, preventing micro-chipping under cyclic shock loads.
- Cobalt Content Balance: A cobalt binder below 6% leaves the tool too brittle to endure the high-frequency shear oscillations of Inconel cutting. Conversely, a cobalt binder exceeding 12% softens at cutting temperatures above 800°C, accelerating crater wear and tool plastic deformation.
2. High-Performance Ceramic Tooling Substrates
When volumetric metal removal is the primary roughing objective, ceramic tooling provides a major advantage over carbide. Ceramics operate on an entirely different metal-cutting paradigm: plasticized thermal shearing.
Rather than cooling the cut, ceramic tooling intentionally runs at extreme surface speeds (600 to 1,200 SFM / 180 to 365 m/min). The extreme localized friction generates temperatures exceeding 1,100°C directly in the shear zone. Because Inconel 718 softens significantly at these temperatures, the material shears easily, lowering specific cutting resistance and dramatically increasing metal removal rates.
- Silicon Carbide Whisker-Reinforced Ceramics (SiCw + Al₂O₃): These substrates utilize an alumina (Al₂O₃3) matrix reinforced with single-crystal silicon carbide whiskers (SiCw). The embedded whiskers act as microscopic composite rebar, deflecting propagating micro-cracks and providing high fracture toughness ((K₁c ≈ 6.0 to 8.5 MPa·m¹/²)), which allows interrupted cuts and milling passes.
- Sialon Ceramics (Si-Al-O-N): For continuous turning operations, Sialon ceramics deliver high thermal shock resistance and chemical stability, resisting notch wear along the depth-of-cut line where the tool interfaces with the oxidized outer crust of raw forgings.
3. PVD Coating Physics
Chemical Vapor Deposition (CVD) coatings generally perform poorly in Inconel milling because the high coating process temperatures (>950°C) degrade the transverse rupture strength of fine-grain carbide substrates and generate tensile residual stresses that encourage crack propagation.
Instead, specify Physical Vapor Deposition (PVD) coatings applied at temperatures below 500°C, which induce beneficial compressive residual stresses in the cutting edge:
- PVD AlCrN (Aluminum Chromium Nitride): AlCrN delivers higher oxidation resistance (withstanding service temperatures up to 1,100°C) and higher thermal stability than standard AlTiN coatings. Under cutting friction, the coating forms an ultra-dense, self-healing chromium oxide (Cr₂O₃) barrier layer that prevents chemical diffusion between the nickel workpiece and the carbide tool.
- PVD TiAlN / AlTiN Multi-Layer Nano-Composites: Alternating nano-layers of TiAlN and AlTiN stop micro-cracks from propagating through the coating matrix. An aluminum content above 65% in the coating matrix promotes aluminum oxide (Al₂O₃) barrier formation along the rake face during cutting.
4. Precision Cutting Edge Preparation (Micro-Honing & T-Lands)
Never use raw, razor-sharp ground cutting edges when machining Inconel 718. Under high mechanical stresses, a razor-sharp edge lacks sufficient structural backing, leading to immediate microscopic chipping.
- Carbide Edge Honing: Apply a precision micro-hone to the cutting edge, establishing a controlled radius (rβ) between 0.015 mm and 0.025 mm (0.0006″ to 0.0010″). A waterfall hone (where the hone radius is larger on the rake face than on the flank face) provides optimal structural support against shear forces without increasing plowing forces.
- Ceramic Edge Preparation (T-Lands): Ceramic inserts must feature a negative chamfer (T-land), typically 0.05 mm to 0.10 mm×20°, combined with a light hone. The negative chamfer redirects cutting forces into compressive stresses within the insert core, where ceramics exhibit their highest mechanical strength.
Cooling Strategies: High-Pressure Coolant vs. Dry Ceramic Cutting
Cooling strategies in Inconel 718 depend entirely on whether you are cutting with solid carbide or ceramic tooling. Applying the wrong cooling method to either substrate will cause immediate tool failure.
Cooling Regimes: Carbide vs. Ceramic Tooling
Inconel 718 Thermal ManagementCarbide Tooling Regime
HPC ProtocolCeramic Tooling Regime
Dry MachiningThe Carbide Regime: High-Pressure Coolant (HPC at 70 to 100 Bar)
Standard external flood coolant delivered at 3 to 5 bar is largely ineffective when roughing Inconel 718 with carbide. At cutting zone temperatures exceeding 900°C, the coolant boils before reaching the cutting edge.
A microscopic vapor barrier (the Leidenfrost Effect) forms, preventing the liquid from wetting the cutting zone. The tool runs hot and dry, and when coolant periodically splashes against the superheated carbide, the resulting thermal shock produces comb-like thermal cracks perpendicular to the cutting edge.
To overcome this, high-performance shops utilize High-Pressure Through-Spindle Coolant (HPC) operating at 70 to 100 bar (1,000 to 1,500 PSI):
- Piercing the Vapor Blanket: High-velocity fluid micro-jets directed through internal tool orifices deliver kinetic momentum that pierces the steam barrier, delivering liquid coolant directly to the wedge between the tool rake face and the chip.
- Thermal Barrier Stabilization: HPC reduces contact-zone temperatures by 150°C to 200°C, keeping the carbide substrate below the thermal threshold where the cobalt binder softens.
- Hydraulic Chip Curling: The concentrated hydraulic force of a 70+ bar fluid jet strikes the underside of the evolving chip, forcing it upward and curling it into tight “C” and “6” configurations that easily eject from deep pockets, preventing chip recutting.
- Coolant Concentration Control: Maintain a strict 10% to 12% concentration of high-lubricity, chlorine-free semi-synthetic or ester-based water-soluble emulsion. Refractometer readings must be logged daily.
The Ceramic Regime: Dry Machining or High-Pressure Compressed Air Blast
When cutting Inconel 718 with whisker-reinforced ceramics, liquid coolant must never be used in continuous operations.
Ceramic substrates have lower thermal conductivity and lower thermal shock resistance than tungsten carbide. If a liquid coolant stream strikes a ceramic insert that is plasticizing material at 1,000°C, the sudden localized temperature drops cause severe thermal contraction. The ceramic substrate experiences thermal shock, cracking and shattering the insert instantly.
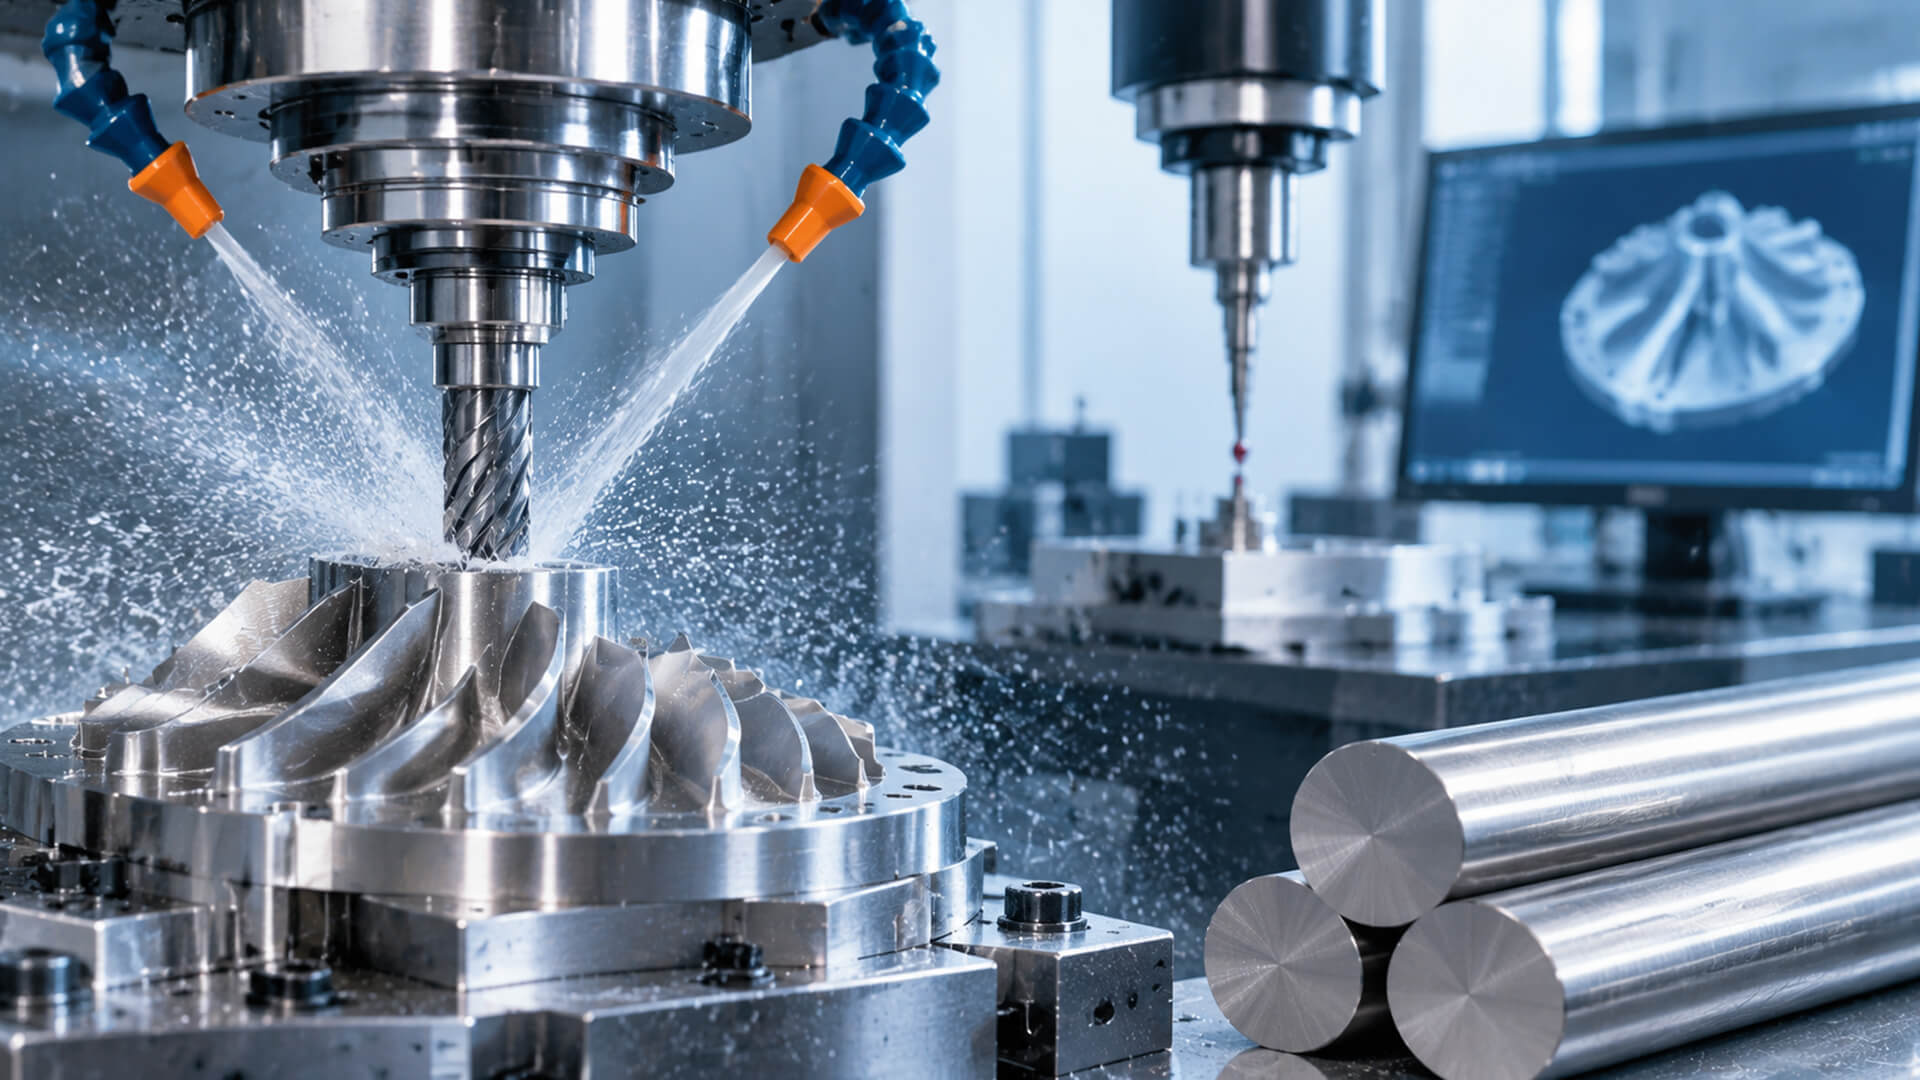
Ceramic cutting must run completely dry or with a clean, dry compressed air blast (6 to 8 bar). The air blast provides no cooling to the cutting zone, which is intentional—the process requires high temperatures to plasticize the Inconel 718. Instead, the high-velocity air blast clears red-hot chips out of the cutting path, preventing them from falling under the cutter and causing mechanical shock fractures.
Machine Rigidity: Why Heavy 5-Axis Platforms Are Mandatory
Inconel 718 possesses high dynamic shear resistance. Cutting forces fluctuate rapidly due to shear localization and serrated chip formation. If the machine tool, spindle bearings, or workholding fixtures lack sufficient dynamic rigidity, these force spikes excite resonant vibration frequencies, causing severe chatter.
In Inconel, minor harmonic chatter leads to immediate tool failure. As the tool vibrates, it repeatedly strikes the workpiece surface, work-hardening the contact zone. The next entering flute impacts this hardened surface, chipping the cutting edge.
Machine Base Damping and Kinematic Platforms
At Celerity Precision, Inconel 718 components are routed across high-damping, high-rigidity machine platforms:
- Mineral-Cast Polymer Concrete Beds: Our German Hermle C400 and DMG MORI DMU 50 5-axis CNC machining centers utilize mineral-cast bases. Polymer concrete provides dynamic structural damping up to 10 times higher than welded steel and significantly higher than standard gray cast iron, absorbing high-frequency harmonics generated by Inconel shearing.
- High-Rigidity Horizontal Centers: For heavy continuous production, our Makino a40 horizontal machining centers feature stepped column castings, twin-driven ball screws, and high-clamping-force pallet interfaces that maintain structural alignment under heavy radial cutting forces.
- Simultaneous 5-Axis Kinematic Advantages: Five-axis kinematics allow tools to be oriented at optimal angles relative to the workpiece, eliminating the need for long-overhang tools. Keeping the tool length-to-diameter ratio (L/D) under 3:1 is critical; cantilever deflection increases with the cube of length (Deflection∝L³).
Tool Overhang Deflection Physics
Deflection ∝ L³High-Torque Toolholding Systems
Standard split-collet chucks (such as ER collets) are unsuited for Inconel 718 milling. High torsional loads and severe micro-vibrations can cause tool micro-creep or pullout, dragging the cutter deeper into the workpiece.
- Thermal Induction Shrink-Fit Chucks: Shrink-fit systems clamp 360 degrees around the ground carbide shank with high radial grip forces. They provide runout under 0.003 mm (0.0001″) measured at 3 × D, combined with exceptional rotational balance (G2.5 at 25,000 RPM).
- Precision Hydraulic Chucks: Hydraulic toolholders feature an internal pressurized fluid chamber that compresses an internal expansion sleeve around the cutter. The fluid acts as an integrated shock absorber, dampening micro-vibrations before they transfer into the spindle bearings, extending carbide tool life in interrupted cuts.
To review our complete production floor capabilities, inspect our precision CNC milling capabilities.
Metallurgical Quality Control & Precision Inspection
Producing aerospace turbine components, hot-section manifolds, and downhole tools from Inconel 718 requires strict quality verification to ensure compliance with material specifications and drawing callouts.
Residual Stress Management and Stress-Relief Annealing
Heavy roughing operations induce steep thermal and mechanical strain gradients within Inconel 718, locking high tensile residual stresses into the sub-surface layers. If a complex thin-walled part is finished immediately after roughing, releasing it from the fixture causes these internal stresses to re-equilibrate, warping the component out of tolerance.
To guarantee long-term dimensional stability:
- Two-Stage Machining Workflow: Rough out the bulk stock, leaving a uniform 0.50 mm to 0.75 mm (0.020″ to 0.030″) stock allowance across all surfaces.
- Intermediate Stress-Relief Annealing: Subject the semi-machined parts to a controlled furnace stress-relief thermal cycle (typically heating at controlled ramp rates to 870°C to 900°C for solution-annealed components, dwelling for 1 to 2 hours, followed by slow cooling) to relieve internal mechanical stresses before performing final semi-finishing and finishing passes.
- Low-Stress Finishing Cuts: Finishing passes must take light, sharp cuts to avoid re-introducing residual surface stresses into the finished part.
Zeiss CMM Dimensional Verification
Dimensional verification of tight-tolerance Inconel 718 features is conducted in Celerity Precision’s climate-controlled quality assurance laboratory, maintained at a continuous 20°C ± 1°C (68°F ± 1.8°F).
- Normalization Soaking: Finished Inconel components must soak inside the metrology lab for 4 to 8 hours to reach thermal equilibrium before probing.
- Zeiss Coordinate Measuring Machines: Using our bridge-type Zeiss CMM equipped with high-accuracy scanning probes, critical features, concentricities, and complex 3D blade surfaces are mapped to verified tolerances down to ±0.005 mm (±0.0002″).
- Surface Integrity Metrology: Optical profilometry and contact stylus profilometers verify that surface finishes comply with engineering requirements (Ra≤0.4μm) without thermal micro-cracking, smearing, or plowing defects.
Raw Material Authentication via XRF Spectroscopy
A significant challenge in sourcing Inconel 718 is the proliferation of off-spec heats, substandard secondary melts, or mislabeled stainless steels (such as 316L or 17-4 PH) entering the supply chain. Substituting an inferior alloy in an aerospace turbine or downhole casing can result in catastrophic in-service structural failure.
Celerity Precision validates incoming raw bar stock, forgings, and plate using an on-site X-Ray Fluorescence (XRF) Spectrometer / Analyzer:
- Chemical Lot Profiling: Every incoming material lot undergoes non-destructive spectroscopic analysis to verify primary elemental ratios:
- Nickel (Ni): 50.00% to 55.00%
- Chromium (Cr): 17.00% to 21.00%
- Niobium + Tantalum (Nb + Ta): 4.75% to 5.50%
- Molybdenum (Mo): 2.80% to 3.30%
- Titanium (Ti): 0.65% to 1.15%
- Aluminum (Al): 0.20% to 0.80%
- Traceability Verification: Real-time XRF spectral fingerprints are cross-referenced directly against mill test reports (MTRs), ensuring complete material traceability from the raw melt to the final shipped part.
DFM Guidelines to Cut Inconel Machining Costs
Inconel 718 raw stock costs 15 to 25 times more than carbon steels, and machining cycle times are substantially longer. Poor Design for Manufacturability (DFM) drives up unit costs through accelerated tool wear, frequent cutter changes, and elevated scrap rates.
Applying these four design guidelines helps balance mechanical performance with realistic manufacturing costs:
1. Limit Pocket Depth-to-Width Aspect Ratios
Specifying deep, narrow pockets forces machine shops to use long-overhang end mills. When tool overhang exceeds L/D>3, feeds and speeds must be reduced by 50% to 70% to avoid chatter, dramatically increasing cycle times.
- DFM Rule: Design pocket depths to ≤3× tool diameter whenever possible. Where deep cavities are unavoidable, incorporate step-downs or draft angles (1° to 3°) to allow tapered, high-rigidity cutters to clear the upper cavity.
2. Maximize Internal Corner Fillet Radii
Designing sharp vertical internal corners (R≤1.5 mm) inside deep cavities creates severe machining bottlenecks. When an end mill cuts into a sharp 90-degree corner, the tool’s radial arc of engagement spikes from 25 degrees to over 110 degrees. In Inconel 718, this sudden engagement spike induces chatter, creates localized work hardening, and frequently breaks the cutter.
- DFM Rule: Specify internal corner radii at least 25% to 30% larger than the roughing cutter radius. For example, if a 10 mm end mill (R=5 mm) clears a pocket, design internal corners with a radius of R≥6.5 mm. This allows the tool to maintain a smooth trochoidal arc through the corner without stopping or experiencing radial engagement spikes.
3. Maintain Generous Wall Thicknesses
Because Inconel 718 exerts high specific cutting forces on the tool and workpiece, thin vertical walls deflect elastically under cutter side-pressure, leading to chatter, wall taper, and dimensional variation.
- DFM Rule: Maintain structural wall thicknesses ≥2.0 mm (0.080″) where possible. If thin aero-style ribs (<1.2 mm) are essential, design structural ribs, support gussets, or broad transition radii at the wall base to maximize local mechanical rigidity during semi-finishing passes.
4. Optimize Thread Depth and Standardize Thread Types
Tapping Inconel 718 with cut taps carries a high risk of tool breakage. The alloy’s elastic recovery closes in behind the tap, pinching the cutting edges and breaking the tool inside the hole.
- DFM Rule: Limit tapped thread depths to 1.5×D (maximum 2.0×D). The first four to five threads carry over 80% of the mechanical tensile load; specifying deeper threads provides negligible mechanical benefit while exponentially increasing tap breakage risk. Where possible, design for thread milling rather than tapping, which allows broken tools to be extracted without scrapping the entire part.
Precision Inconel Manufacturing for Aerospace & Energy Components
Machining Inconel 718 successfully requires deep metallurgical knowledge, high-rigidity 5-axis and horizontal machine kinematics, disciplined feeds and speeds, high-pressure coolant delivery, and climate-controlled metrology.
Whether your application calls for structural components produced on our 5-axis CNC machining centers or complex turn-mill parts supported by our custom Inconel CNC machining services, Celerity Precision delivers repeatable, flight-critical components backed by complete material certifications and Zeiss CMM inspection reports.
Request a Comprehensive DFM Review and Inconel Quotation
Submit your 3D CAD models (STEP, IGS) and 2D engineering drawings to our aerospace applications team. We will deliver an engineering-grade manufacturability review within 24 hours, detailing optimal tooling strategies, stress-relief allowances, GD&T tolerance feasibility, and transparent factory-direct pricing.
- Strict Non-Disclosure Agreement (NDA) Protection
- 24-Hour Engineering DFM & Quotation Turnaround
- Full Material Traceability & Zeiss CMM Dimensional Inspection
Upload your CAD files via our contact page to begin your project review with our engineering team.

CP Engineering Team
Authored and peer-reviewed by the Senior Engineering and Metrology Team at Celerity Precision. Backed by German 5-axis CNC machining centers, high-speed micro-milling platforms, and a climate-controlled Zeiss CMM inspection lab, our team delivers deep DFM insights, material machinability guides, and precision manufacturing solutions for aerospace, medical, and semiconductor developers worldwide.